What Is Poka Yoke in Screwdriving and How Does It Prevent Assembly Errors
In precision manufacturing, automotive components, 3C electronics, new energy systems and other quality-critical industries, fastening errors can lead to rework, lower first-pass yield and field failures. Common problems include missed screws, incorrect screws, incomplete tightening, repeated tightening and torque deviations.
Traditional screwdriving processes often depend heavily on operator technique and manual inspection. This makes quality vulnerable to fatigue, distraction and inconsistent work methods. Poka Yoke, or mistake-proofing, moves quality control into the fastening process itself. By combining controlled hardware, programmed logic and real-time process monitoring, manufacturers can prevent many errors before they occur, detect abnormalities as they happen and stop nonconforming assemblies from moving downstream.
Quick Answer
Poka Yoke in screwdriving is a process-control approach that makes fastening mistakes difficult to perform and difficult to pass unnoticed. An intelligent tightening system can verify torque, angle, screw count, tightening sequence and process results, then trigger an alarm or interlock when an operation falls outside the defined process window.
What Is Poka Yoke in Screwdriving
Poka Yoke is a mistake-proofing concept associated with Japanese lean manufacturing. Its purpose is to reduce dependence on subjective judgment and continuous operator attention. In screwdriving, the method uses equipment controls, tightening programs, process limits and system interlocks to prevent an incorrect action or identify it immediately.
Unlike end-of-line inspection, screwdriving Poka Yoke creates a closed-loop quality process that covers prevention before tightening, control during tightening and traceability after tightening. The approach is built on three principles:
1 Prevent errors before tightening. Access control, program selection, parameter matching and process logic restrict operations that do not belong to the defined assembly process.
2 Detect abnormalities in real time. Sensors and dynamic torque and angle monitoring capture abnormal conditions such as missed fastening points, incomplete seating, incorrect parameters or unexpected joint behavior.
3 Stop and record nonconforming results. When the system detects an abnormal result, it can stop the operation, interlock the station, activate an alarm and save the relevant tightening data for review.
The practical objective is to reduce operator-related variation and standardize fastening quality through an intelligent, controlled process that supports zero-defect manufacturing goals.
Five Common Screwdriving Errors That Poka Yoke Helps Control
In high-volume assembly, many fastening defects result from repeatable process and operating errors rather than a failure of the tightening tool itself. The following five error types are common targets for a screwdriving mistake-proofing system.
1 Missed Screws
A single workstation may contain several fastening points. Fast line speeds and operator fatigue can result in an incomplete screw count. A missing screw may weaken the product structure, compromise sealing performance or allow components to loosen. Screw-count control and station interlocks help ensure that all required fastening points are completed before release.
2 Incorrect Screws
Precision assembly stations may use screws with different lengths, pitches, materials or specifications. Manual picking creates a risk of mixing components, such as inserting a smaller screw into a larger hole or substituting a nonstandard screw. This can reduce assembly accuracy and create long-term reliability concerns.
3 Incomplete Tightening and Overtightening
An uncontrolled manual tool may not apply the required torque consistently. Insufficient torque can leave a screw incompletely seated and vulnerable to loosening. Excessive torque can damage threads, strip the screw or crack and deform the workpiece. These conditions are particularly difficult to control in electronics and automotive component assembly.
4 Repeated Tightening
During manual inspection or rework, an already accepted screw may be tightened again. Repeated loading can fatigue the fastener, damage the thread and reduce product life. Process completion records and point-by-point guidance help prevent unnecessary repeat operations.
5 Incorrect Tightening Sequence
Multi-point assemblies may require a defined sequence, especially for cross-pattern tightening, staged fastening and enclosure sealing. Changing the sequence can create uneven loading, residual stress, deformation and reduced structural stability.
How Danikor Tightening Tools Apply Poka Yoke
Danikor intelligent tightening tools integrate mistake-proofing functions for automated production lines, semi-automatic workstations and precision manual assembly. The system addresses missed operations, incorrect fastening, abnormal process parameters and traceability requirements through the following capabilities.
Torque and Angle Monitoring for Incomplete or Excessive Tightening
A final torque value alone may not reveal how the joint behaved during tightening. Danikor tools combine torque and angle monitoring so the system can evaluate two process dimensions against a defined tightening program.
Application-specific torque and angle limits can be configured in advance. During the cycle, the controller compares the measured result with the programmed process window. Insufficient torque or angle may indicate incomplete tightening, while excessive torque or rotation may indicate overtightening or another abnormal joint condition. When a result falls outside the limits, the system can stop the cycle, produce an alarm and retain the abnormal result for analysis.
This approach is suited to quality-critical applications such as new energy batteries, automotive fasteners and precision components, where the final result and the tightening process both require verification.

Danikor intelligent tightening tool with real-time torque, angle and OK result display.
Program Logic for Tightening Sequence and Point Control
For cross-pattern tightening, staged fastening, sealed assemblies and other sequence-sensitive processes, Danikor tools can work with graphical guidance software to define fastening points and the required operating order.
The software guides the operator through the programmed sequence. If one point has not achieved an accepted tightening result, the next point cannot proceed. This helps prevent uneven stress, deformation and loss of assembly accuracy caused by an incorrect sequence. Program matching and process controls can also restrict nonstandard fastening actions and reduce the risk of using the wrong screw or tightening program.
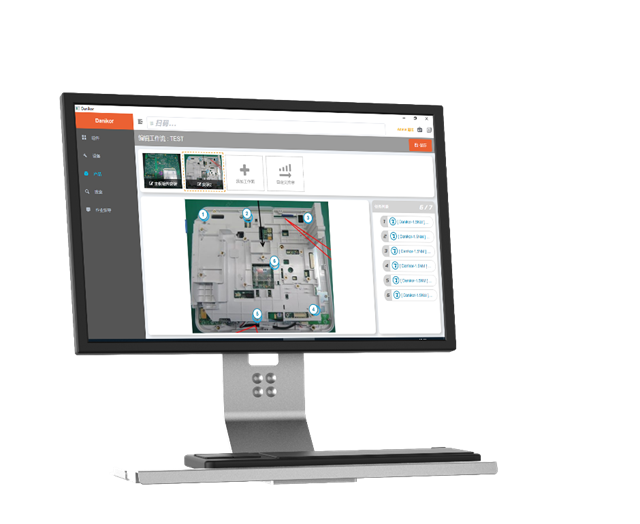
Graphical work guidance supports point-by-point sequence control and process confirmation.
Fastening Data Traceability for Closed Loop Quality Control
Danikor tightening systems can collect and store process data for each fastening cycle, including torque, angle, cycle time, OK/NG status and tool identification. Results can be retained locally and retrieved for production review.
The system can also connect with MES or ERP platforms to support centralized data management. If a product quality issue occurs, recorded results can help the manufacturer trace the fastening history of an individual screw, analyze the likely cause and identify the affected process. This creates a quality loop in which operations are monitored, abnormalities are flagged and fastening results remain traceable.
Business and Manufacturing Value of Screwdriving Error Proofing
As manufacturers focus on quality, cost and throughput, Poka Yoke has become an important process requirement for precision fastening rather than an optional add-on. A controlled tightening system can create value in four areas.
1 Reduce human error and support defect prevention. Programmed process logic and real-time monitoring reduce dependence on operator memory, attention and individual technique. This helps control missed screws, incorrect screws, incomplete tightening, overtightening and repeated tightening.
2 Reduce quality costs and improve workflow. Earlier detection can reduce rework, scrap and after-sales service costs. Automated verification can also reduce the need for separate manual inspection and support more predictable station cycle times.
3 Standardize the tightening process. Defined programs replace inconsistent work methods with common torque, angle, sequence and acceptance criteria across the production line, improving batch-to-batch consistency.
4 Support quality-critical manufacturing. Detailed fastening records help automotive, new energy, precision electronics and industrial-control manufacturers prepare for customer quality reviews and strengthen product-level traceability.
Poka Yoke Makes Tightening Quality Controllable and Traceable
Many fastening defects are linked to inconsistent operations and process deviations rather than a hardware failure. Poka Yoke addresses this risk by replacing uncertain manual decisions with standardized, digital process controls.
For screwdriving, the most effective mistake-proofing strategy does more than check whether a torque value was reached. It confirms that the correct program was used, each required point was completed, the tightening sequence was followed, torque and angle stayed within the process window, and the result was recorded. This is how intelligent tightening helps prevent hidden assembly defects at the source and stops abnormal results from moving to the next production stage.
Frequently Asked Questions About Poka Yoke in Screwdriving
What does Poka Yoke mean in screwdriving?
It means designing the fastening process to prevent mistakes or detect them immediately. Typical controls include program selection, screw-count verification, sequence control, torque and angle monitoring, OK/NG judgment and station interlocks.
Can torque control alone prevent all tightening errors?
No. A final torque value may not show whether the screw followed a normal tightening path. Combining torque with angle, sequence, count and process-window monitoring gives a more complete view of the fastening cycle.
How can a tightening system prevent missed screws?
The system can count accepted tightening cycles for each product and prevent the workstation from releasing the assembly until every required fastening point has returned an OK result.
How does graphical work guidance improve fastening quality?
It shows the operator which point to tighten next and links tool activation to the programmed sequence. This reduces skipped points, repeated tightening and incorrect operating order.
What tightening data can be traced?
Depending on the configured system, records can include torque, angle, cycle time, OK/NG status, program, tool identification and product or station information.
Can Danikor tightening tools connect to MES or ERP systems?
Danikor tightening systems can be configured for production-system integration. The exact communication method and data fields should be confirmed for the selected controller, software and plant architecture.
Where is screwdriving Poka Yoke commonly used?
Typical applications include automotive assembly, automotive components, EV batteries and powertrain systems, energy storage, 3C electronics, industrial controls and other quality-critical manufacturing processes.